Rear Fender Installation - Ar63.50-P-1400-04RG
 |
000 588 04 39 00 Rivet press tool |
|
WS60.00-P-0440B |
|
000 588 12 84 00 Welder |
|
WS00.00-P-0318K |
Model 190.3
GAP DIMENSIONS
| Number |
Designation |
Model 190.3 |
| BE60.00-P-1008-01EA |
Gap dimension, sidewall panel to door paneling |
Dimension "H" |
mm |
3, 5 (±0, 5) |
| See |
|
AR60.00-P-0700-01RG |
GAP DIMENSIONS
| Number |
Designation |
Model 190.3 |
| BE60.00-P-1009-01EA |
Gap dimension, longitudinal member panel to fender/sidewall panel |
Dimension "I" |
mm |
0 (+0, 5) |
| See |
|
AR60.00-P-0700-01RG |
GAP DIMENSIONS
| Number |
Designation |
Model 190.3 |
| BE60.00-P-1020-01EA |
Gap dimension, side wall paneling to tailgate/trunk lid/rear spoiler |
Dimension "T" |
mm |
3, 5 (±0, 5) |
| See |
|
AR60.00-P-0700-01RG |
GAP DIMENSIONS
| Number |
Designation |
Model 190.3 |
| BE60.00-P-1021-01EA |
Gap dimension, sidewall panel to taillamp |
Dimension "U" |
mm |
1 (±1) |
| See |
|
AR60.00-P-0700-01RG |
GAP DIMENSIONS
| Number |
Designation |
Model 190.3 |
| BE60.00-P-1023-01EA |
Gap dimension, tank cap |
Dimension "W" |
mm |
2, 5 (±0, 5) |
| See |
|
AR60.00-P-0700-01RG |
GAP DIMENSIONS
| Number |
Designation |
Model 190.3 |
| BE60.00-P-1026-01EA |
Gap dimension, sidewall panel to bumper |
Dimension "Z" |
mm |
0, 5 (±0, 5) |
| See |
|
AR60.00-P-0700-01RG |
 Courtesy of MERCEDES-BENZ USA
REPAIR MATERIALS
| Number |
Designation |
Order number |
| BR00.45-Z-1012-13A |
Blind rivet Y2 6.5x12.5 (clamping range 2 mm to 5 mm, draw-off strength min. 19 kN) |
A 004 990 16 97 |
| BR00.45-Z-1026-13A |
Flow-form rivet structure W1 up to 3.5 mm clamping range (S1) |
A 000 991 11 33 |
| BR00.45-Z-1048-13A |
Flow-form rivet structure 1.3 mm up to 2.5 mm clamping range (S08) |
A 000 991 23 33 |
| BR00.45-Z-1162-02A |
Parts kit for 2-component adhesive for body |
A 012 989 17 71 |
 Further information can be found in the superordinate service document. Comply with safety information in superordinate customer service document.
The following operation steps are shown on the left side of the vehicle. This must be similarly performed for damage to the right side.
When MIG welding ( ) prepare welds by grinding down to bare metal with stainless steel brush. Tack weld seams at start, end and approx. every 4 cm. The weld seam gap must not be larger than 1 mm; if necessary, make a preseam.
Replace flow drill screws installed on the vehicle with high-strength rivets.
- Install and fit welding bath support, rear fender (1), lock striker, door, tailgate, rear lamp units, rear bumper, and seals.
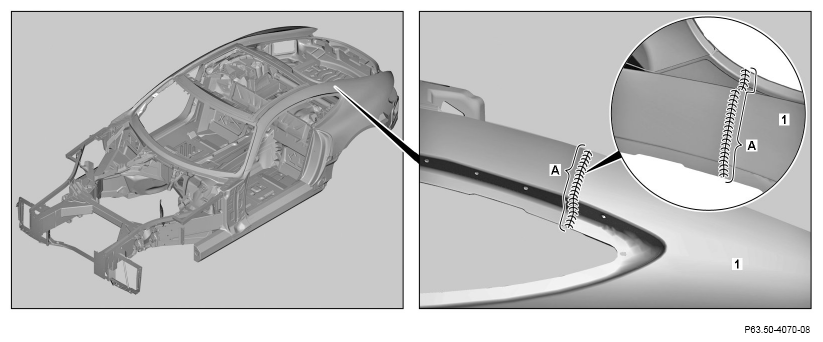
Insert welding bath support between side roof paneling and rear fender (1) and align in center (area A).
- Check gap dimensions using
 feeler gauge and adjust if necessary.
- Fix rear fender (1) in place.
- Remove door, lock striker, tailgate, rear lamp units, rear bumper, and seals.
 Courtesy of MERCEDES-BENZ USA
|
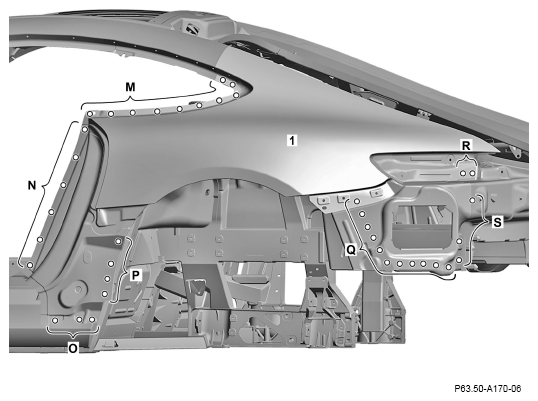
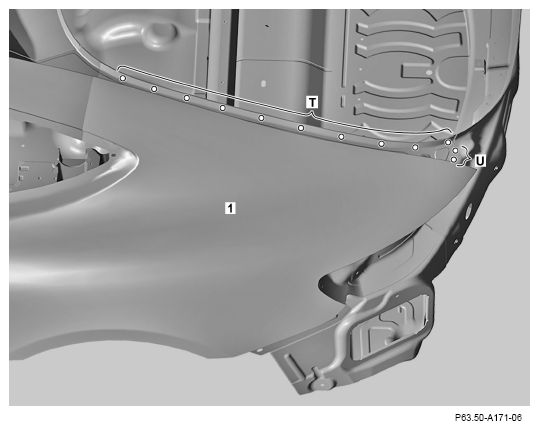
- Drill rivet holes in rear fender (1) with a diameter of 6.7 mm (areas O, P, Q, R, S, and U).
If holes are present for flow drill bolts on the vehicle transfer them to new parts. In the case of new part to new part connections, adapt them and drill through together.
- Prepare rear fender (1) with a rivet press tool (areas N, M, and T).
Transfer present positions for rivet connections from vehicle to new part. In the case of new part to new part connections, adapt these and prepare together.
- Remove rear fender (1).
- Deburr rivet holes on rear fender (1) and body on both sides.
Observe pretreatment of bonding surfaces.
- Remove grinding and drill shavings using a wet/dry vacuum cleaner.
 Courtesy of MERCEDES-BENZ USA
|
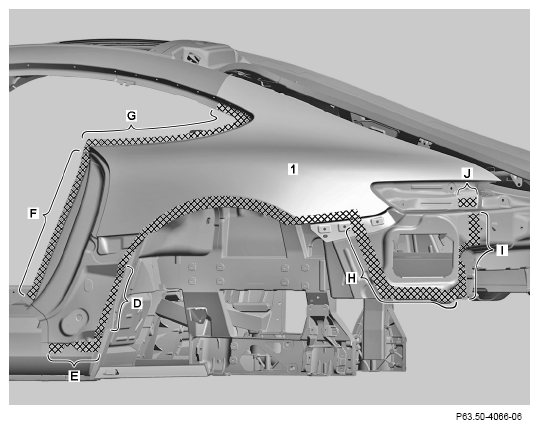
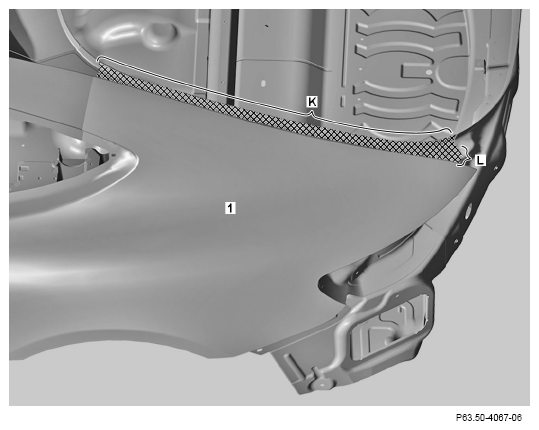
- Apply 2-component adhesive in cross-hatched areas (areas D, E, F, G, H, I, J, K, L).
Refer to the manufacturer's information for the curing and working times of 2-component adhesive.
- Install rear fender (1) and fix in place.
Ensure that weld bath support is seated correctly (area A).
 Courtesy of MERCEDES-BENZ USA
|
 Courtesy of MERCEDES-BENZ USA
|
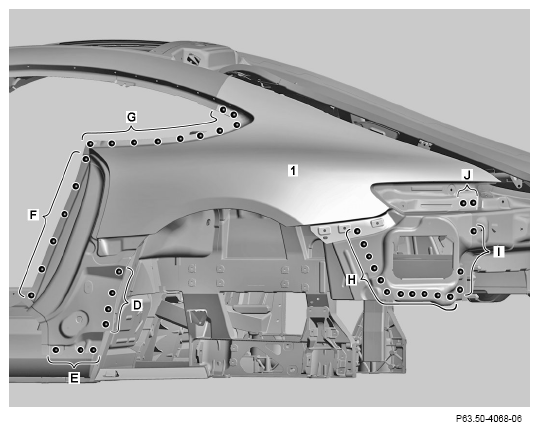
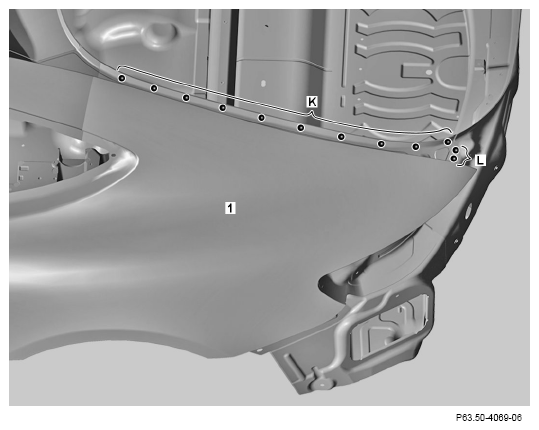
- Rivet rear fender (1) with blind rivets (areas D, E, H, I, J, L).
Use ø 6.5x12.5 blind rivets.
- Rivet rear fender (1) with flow-form rivets (areas F, G, K).
Use flow-form rivet (S08) with a clamping range between 1.30 mm and 2.50 mm (area F).
Use flow-form rivet (S1) with a clamping range between 2.30 mm and 3.50 mm (areas G, K).
 Courtesy of MERCEDES-BENZ USA
|
 Courtesy of MERCEDES-BENZ USA
|
 Courtesy of MERCEDES-BENZ USA
|
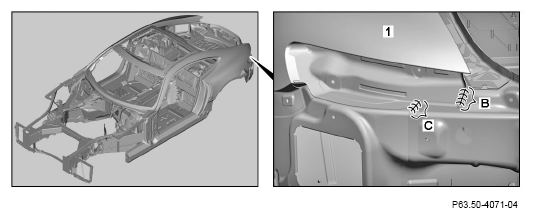
- Rear fender (1)
(areas A, B, C).
Use welding bath support during welding (area A).
- Level weld seams and restore surfaces (areas A, B, C).
- Remove shavings using wet/dry vacuum cleaner.
 Courtesy of MERCEDES-BENZ USA
|