Radiator Support Installation - Ar62.30-P-1500-03RG
 |
000 588 12 84 00 Welder |
|
WS00.00-P-0318K |
Model 190
GAP DIMENSIONS
| Number |
Designation |
Model 190.3 |
Model 190.4 |
| BE60.00-P-1001-01EA |
Gap dimension, engine hood to bumper |
Dimension "A" |
mm |
3, 5 (±0, 5) |
3, 5 (±0, 5) |
| See |
|
AR60.00-P-0700-01RG |
AR60.00-P-0700-01RG |
GAP DIMENSIONS
| Number |
Designation |
Model 190.3 |
Model 190.4 |
| BE60.00-P-1002-01EA |
Gap dimension, fender to engine hood |
Dimension "B" |
mm |
3, 5 (±0, 5) |
3, 5 (±0, 5) |
| See |
|
AR60.00-P-0700-01RG |
AR60.00-P-0700-01RG |
GAP DIMENSIONS
| Number |
Designation |
Model 190.3 |
Model 190.4 |
| BE60.00-P-1003-01EA |
Gap dimension, fender to lamp unit |
Dimension "C" |
mm |
2, 5 (±1) |
3 (±0, 5) |
| See |
|
AR60.00-P-0700-01RG |
AR60.00-P-0700-01RG |
GAP DIMENSIONS
| Number |
Designation |
Model 190.3 |
Model 190.4 |
| BE60.00-P-1004-01EA |
Gap dimension, lamp unit to bumper |
Dimension "D" |
mm |
2, 5 (±1) |
2, 5 (±0, 5) |
| See |
|
AR60.00-P-0700-01RG |
AR60.00-P-0700-01RG |
GAP DIMENSIONS
| Number |
Designation |
Model 190.3 |
Model 190.4 |
| BE60.00-P-1005-01EA |
Gap dimension, fender to bumper lamp unit |
Dimension "E" |
mm |
0 (+0, 5) |
0 (+0, 5) |
| See |
|
AR60.00-P-0700-01RG |
AR60.00-P-0700-01RG |
GAP DIMENSIONS
| Number |
Designation |
Model 190.3 |
Model 190.4 |
| BE60.00-P-1007-01EA |
Gap dimension, fender to door paneling |
Dimension "G" |
mm |
4 (±0, 5) |
4 (±0, 5) |
| See |
|
AR60.00-P-0700-01RG |
AR60.00-P-0700-01RG |
 Courtesy of MERCEDES-BENZ USA
 Courtesy of MERCEDES-BENZ USA
 Courtesy of MERCEDES-BENZ USA
 Further information can be found in the superordinate service document. Comply with safety information in superordinate customer service document.
The following operation steps are shown on the left side of the vehicle. Perform in same manner on right side of the vehicle.
- Install and fit radiator carrier (1) with supports, cross struts, supports and brackets.
 Install welding device.
When working on right side of vehicle, use
supplementary set in addition.
- Install and fit both fenders, lamp units, front bumper and hood.
- Check gaps using
feeler gauge and adjust.
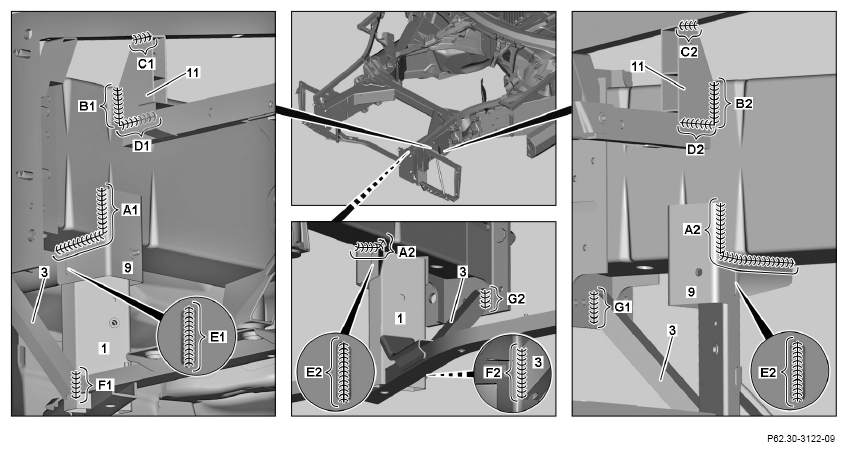
- Fix in place radiator carrier (1) with supports, cross struts, supports and brackets and tack weld with welder (
 ) (areas A1, A2, B1, B2, C1, C2, D1, D2, E1, E2, F1, F2, G1, G2, H1, H2, H3, H4, H5, I1, I2 and I3).
When MIG welding (
) prepare welds by grinding down to bare metal with stainless steel brush. Tack weld seams at start, end and approx. every 4 cm.
- Remove both fenders, lamp units, front bumper and hood.
- Check weld seam gap.
The weld seam gap must not be larger than 1 mm; if necessary, make an add-on seam weld.
 Courtesy of MERCEDES-BENZ USA
|
- Weld radiator carrier (1), left supports (3 and 9) and left upper support (11) with welder (
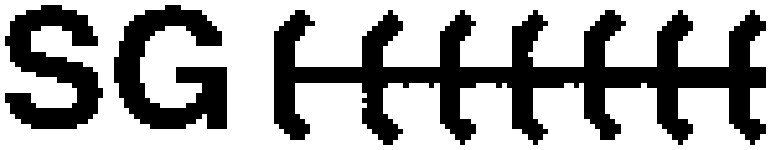 ) (areas A1, A2, B1, B2, C1, C2, D1, D2, E1, E2, F1, F2, G1, G2).
When MIG welding (
), prepare welds by grinding down to bare metal with stainless steel brush directly before welding. Tack weld seams at start, end and approx. every 4 cm. Weld seam gap should not be greater than 1 mm; if required, create a pre-seam.
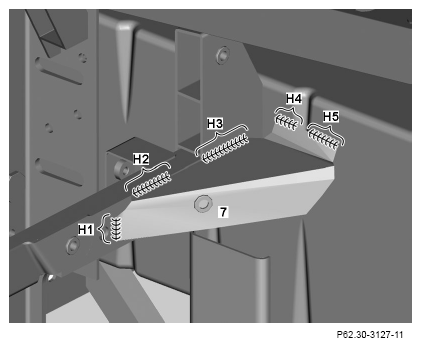
- Weld left upper bracket (7) with welder (
) (areas H1, H2, H3, H4, H5).
When MIG welding (
), prepare welds by grinding down to bare metal with stainless steel brush directly before welding. Tack weld seams at start, end and approx. every 4 cm. Weld seam gap should not be greater than 1 mm; if required, create a pre-seam.
 Courtesy of MERCEDES-BENZ USA
|
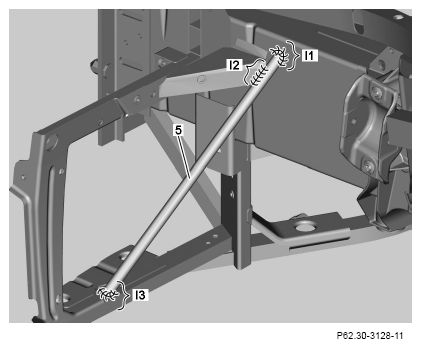
- Weld left cross strut (5) with welder all the way around (
) (areas I1, I3).
When MIG welding (
), prepare welds by grinding down to bare metal with stainless steel brush directly before welding. Tack weld seams at start, end and approx. every 4 cm. Weld seam gap should not be greater than 1 mm; if required, create a pre-seam.
- Weld left cross strut (5) with welder (
) (area I2).
When MIG welding (
), prepare welds by grinding down to bare metal with stainless steel brush directly before welding. Tack weld seams at start, end and approx. every 4 cm. Weld seam gap should not be greater than 1 mm; if required, create a pre-seam.
-
Remove welding device.
When working on right side of vehicle, remove
supplementary set in addition.
 Courtesy of MERCEDES-BENZ USA
|