Piston: Testing and Inspection
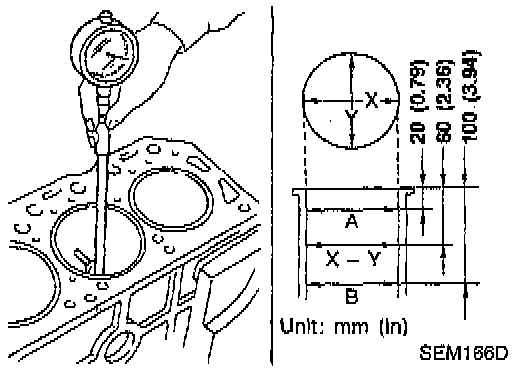
1. Using a bore gauge, measure cylinder bore for wear, out-of-round and taper. The standard inner diameter "Db" is 76.000 - 76.010 mm (2.9921 - 2.9925 inch). The wear limit is 0.2 mm (0.008 inch). Out-of-round (X - Y) is 0.015 mm (0.0006 inch). Taper is (A - B and A - C) 0.01 mm (0.0004 inch). If it exceeds the limit, rebore all cylinders. Replace cylinder block if necessary.
2. Check for scratches and seizure. If seizure is found, hone it.
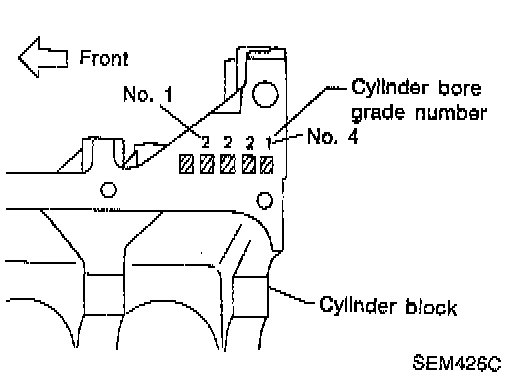
NOTE: If both the cylinder block and pistons are replaced with new ones, select pistons of the same grade numbers as those punched on cylinder block lower surface.

3. Measure the piston skirt diameter and refer to specifications. The measuring point "a" (distance from the bottom) is 9.9 mm (0.390 inch).
4. Check that the piston-to-bore clearance is within specification. Piston-to-bore clearance is 0.015 - 0.035 mm (0.0006 - 0.0014 inch).
5. Determine the piston oversize according to amount of cylinder wear. Oversize pistons are available for service.
6. Cylinder bore size is determined by adding piston-to-bore clearance to piston diameter "A". Rebored size calculation formula is D = A + B - C where, D is the bored diameter; A is the piston diameter as measured; B is the piston-to-bore clearance and C is the honing allowance 0.02 mm (0.0008 inch).
7. Install main bearing cap and tighten bolts to 46.1 - 52.0 Nm (34.00 - 38.36 ft. lbs.). This will prevent distortion of cylinder bores.
8. Cut cylinder bores.
NOTE: When any cylinder needs boring, all other cylinders must also be bored. Do not cut too much out of cylinder bore at a time. Cut only 0.05 mm (0.0020 inch) at a time.
9. Hone cylinders to obtain specified piston-to-bore clearance.
10. Measure finished cylinder bore for out-of-round and taper. Measurements should be taken after cylinder bore cools down.