- Scribe cut on A-pillar (1) and cut (area A).
 Do not cut too deeply. Otherwise the components below can be damaged and weakened.
 To mark the separation line (area A) the dimension (a) must not exceed 370 mm.
- Scribe cut on A-pillar (1) and cut (area B).
Cut through A-pillar (1) and inner A-pillar (area B).
- Scribe cut on A-pillar (1) and cut (area C).
Do not cut too deeply. Otherwise the components below can be damaged and weakened.
- Scribe cut on A-pillar (1) and cut (area D).
Do not cut too deeply. Otherwise the components below can be damaged and weakened.
Cut through A-pillar (1) and longitudinal member reinforcement (area D).
 Courtesy of MERCEDES-BENZ USA
|
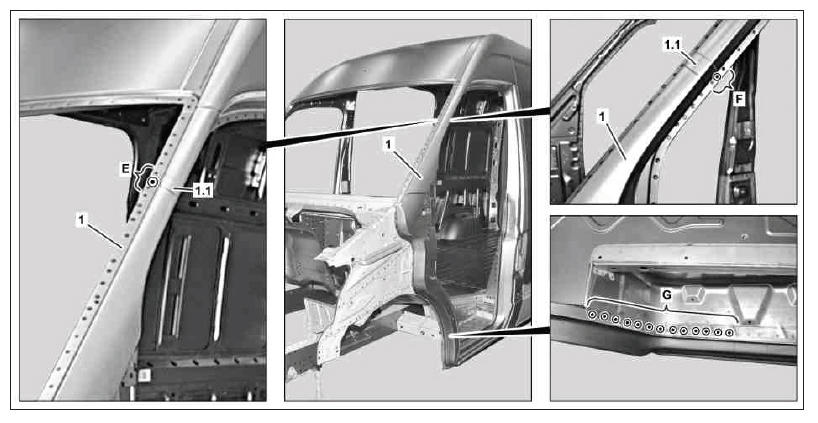
- Expose spot welds on A-pillar (1) and cut out (areas E, F and G).
- Remove section (1.1).
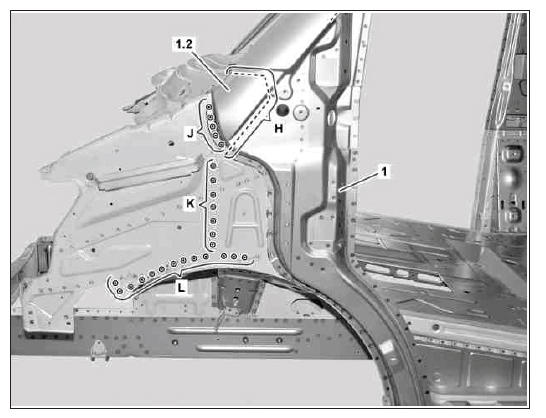
- Expose spot welds on A-pillar (1) and cut out (areas J, K and L).
- Scribe cut on A-pillar (1) and cut (area H).
Do not cut too deeply. Otherwise the components below can be damaged and weakened.
- Remove section (1.2).
 Courtesy of MERCEDES-BENZ USA
|
 Courtesy of MERCEDES-BENZ USA
|
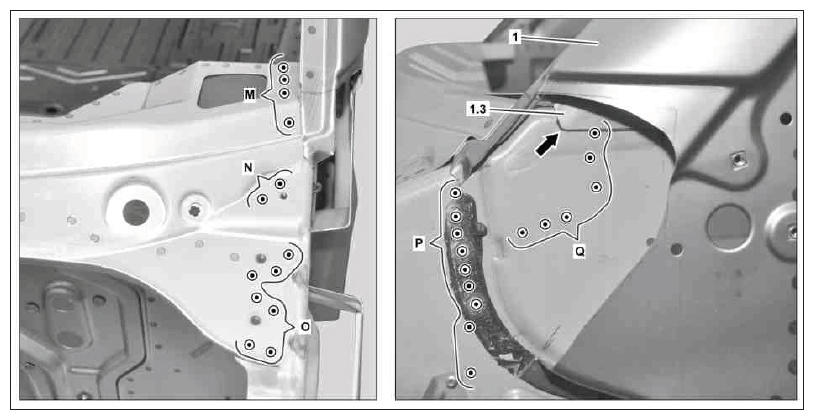
- Pry open sheet metal lug (1.3) in direction of arrow.
- Expose spot welds on A-pillar (1) and cut out (areas M, N, O, P and Q).
Cut out spot welds through two panel thicknesses (area N). It is necessary to feel some of the spot welds from the inside (area Q).
 Courtesy of MERCEDES-BENZ USA
|
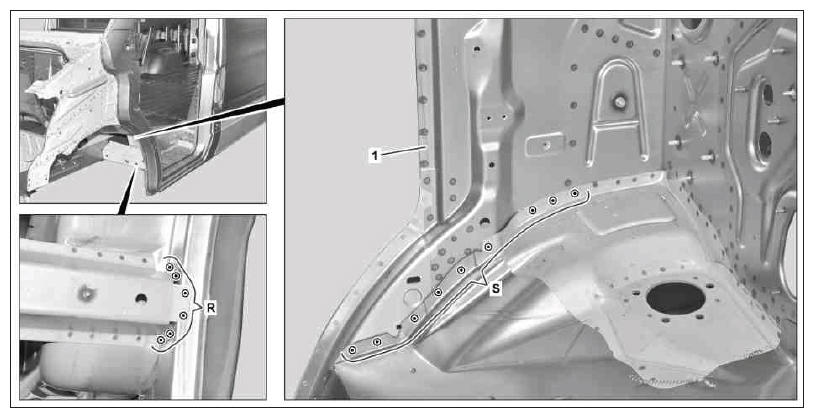
- Expose spot welds on A-pillar (1) and cut out (areas R and S).
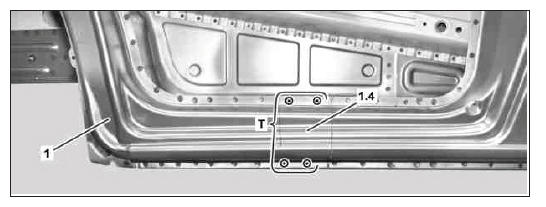
- Expose spot welds on A-pillar (1) and cut out (area T).
- Remove section (1.4).
- Remove damaged A-pillar (1).
 Courtesy of MERCEDES-BENZ USA
|
 Courtesy of MERCEDES-BENZ USA
|
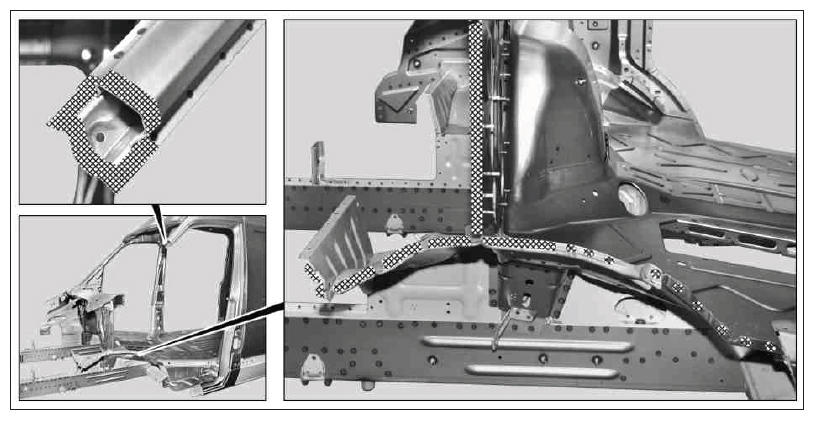
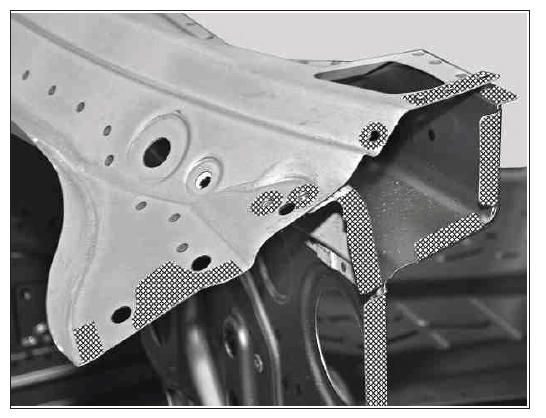
- Grind mating surfaces down to bare metal in the crosshatched areas.
Grind spot weld flanges down to bare metal on both sides.
- Remove drilling chips/savings.
- Coat inside of spot welding flanges with zinc dust paint.
- Grind mating surfaces down to bare metal in the crosshatched areas.
Grind spot weld flanges down to bare metal on both sides.
- Remove drilling chips/savings.
- Coat inside of spot welding flanges with zinc dust paint.
 Courtesy of MERCEDES-BENZ USA
|
 Courtesy of MERCEDES-BENZ USA
|
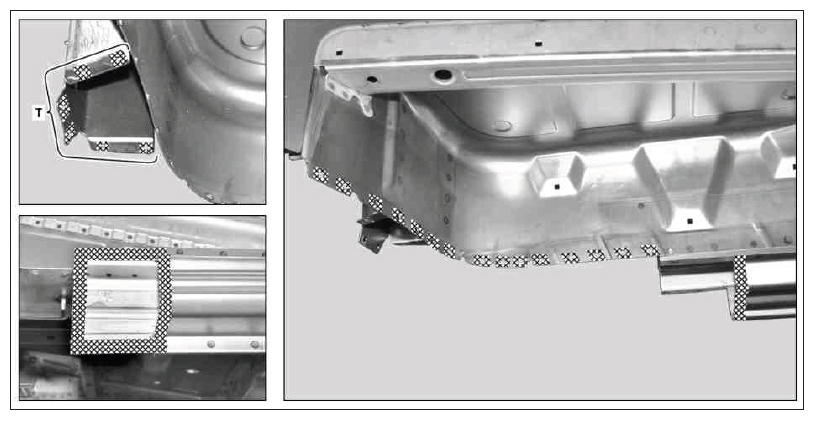
- Grind mating surfaces down to bare metal in the crosshatched areas.
Grind spot weld flanges down to bare metal on both sides. Grind down to bare metal from inside (area T).
- Remove shavings and drill chips.
- Coat insides of spot weld flanges with zinc dust paint.