Prepare B-pillar for installation - AR63.20-P-1350-07SX
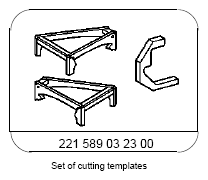 Courtesy of MERCEDES-BENZ USA
COMMERCIALLY AVAILABLE TOOLS
| Number |
Designation |
| WH58.30-Z-1008-01A |
BTR Usibor milling cutter, dia. 8 mm |
| WH58.30-Z-1009-01A |
BTR Usibor milling cutter, dia. 8 x44 mm |
| WH58.30-Z-1010-01A |
BTR Usibor center punch Ø 8 x80 mm |
| WH58.30-Z-1001-03A |
Round wire brush, braided, dia. 70 mm |
| WH58.30-Z-1021-04A |
Cutting disk, dia. 65 mm, 80 m/s (max. 23, 500 RPM) |
| WH58.30-Z-1024-04A |
Abrasive disk, dia. 115 mm, 80 m/s (max. 13, 250 RPM) |
WORKSHOP EQUIPMENT
| WE58.40-Z-1001-03A |
Drill (electric/pneumatic) |
| WE58.40-Z-1002-03A |
Straight grinder (electric/pneumatic) |
| WE58.40-Z-1003-03A |
Angle grinder (electric/pneumatic) |
| WE58.40-Z-1004-03A |
Body saw (electric/pneumatic) |
 Courtesy of MERCEDES-BENZ USA
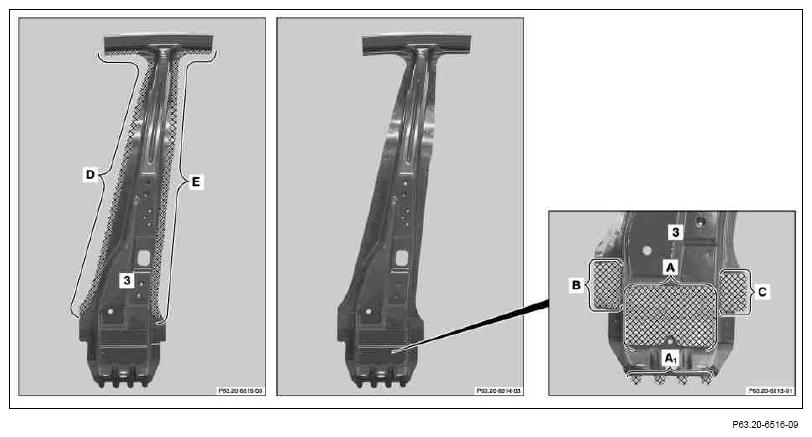
- Grind mating surfaces on B-pillar reinforcement (3) down to bare metal in cross-hatched areas using
 round wire brush (areas A, B, C, D and E).
 Grind B-pillar reinforcement (3) down to bare metal in cross-hatched areas using
round wire brush, on both sides (area A1
).
 To prevent adhesion problems, do not coat bonding surfaces with zinc dust paint. (areas A, A1
, B, C, D and E).
Observe pretreatment of bonding surfaces.
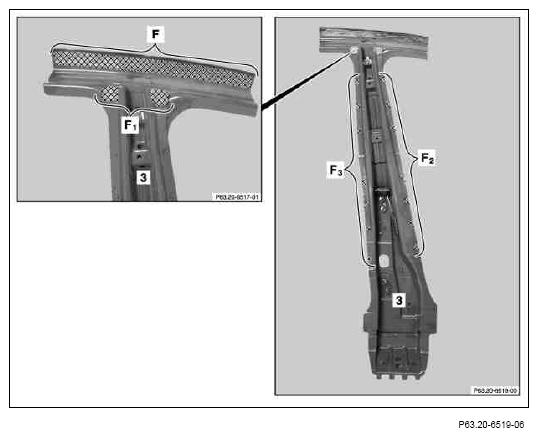
- Grind mating surfaces on B-pillar reinforcement (3) down to bare metal in cross-hatched areas using
round wire brush (areas F and F1).
- Grind spot weld flange on B-pillar reinforcement (3) down to bare metal (areas F2
and F3
).
To prevent adhesion problems, do not coat bonding surfaces with zinc dust paint. (areas F, F1
, F2
and F3
).
Observe pretreatment of bonding surfaces.
 Courtesy of MERCEDES-BENZ USA
 Courtesy of MERCEDES-BENZ USA
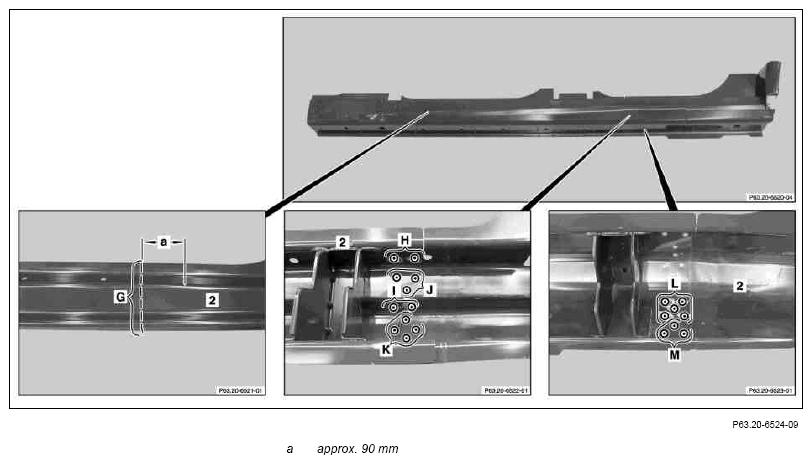
Dimensions:
- Scribe separation line on outer longitudinal member (2) (area G).
- Cut separation point on outer longitudinal member (2) with straight cutter (area G).
- Expose spot welds on outer longitudinal member (2) (areas H, I, J, K, L and M).
- Cut out spot welds on outer longitudinal member (2) using
BTR Usibor milling cutter, dia. 8 x44 mm or
BTR Usibor milling cutter, dia. 8 mm (areas H, I, J, K, L and M).
 Courtesy of MERCEDES-BENZ USA
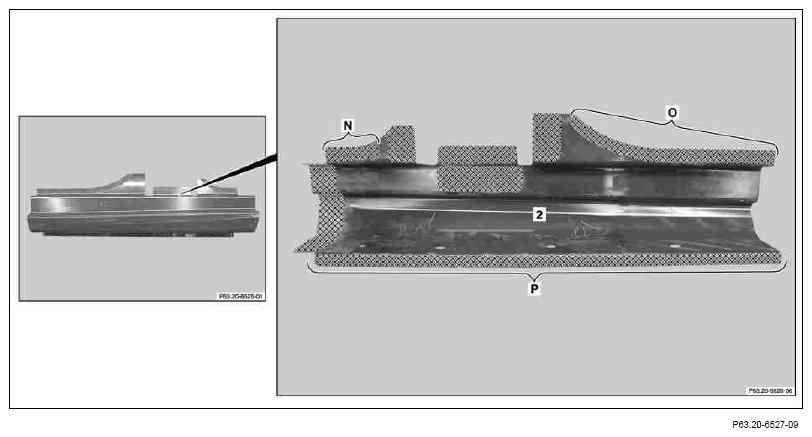
- Grind mating surfaces in cross-hatched areas down to bare metal using
round wire brush.
Grind spot weld flange down to bare metal on both sides (areas N, O and P).
To prevent adhesion problems, do not coat bonding surfaces with zinc dust paint. (areas N, O and P).
Observe pretreatment of bonding surfaces.
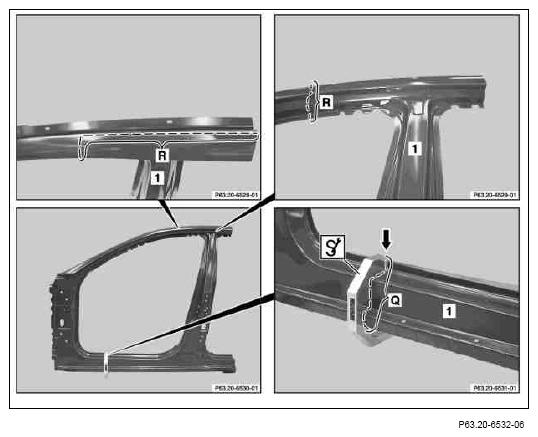
- Scribe separation line on B-pillar outer paneling (1) (area R).
Transfer separation line on B-pillar outer paneling (1) from vehicle.
- Scribe separation lines on B-pillar outer paneling (1) with
 cutting template (area Q).
Position cutting template on Y-marking. Expose Y-marking if necessary (arrow).
- Cut cutting points on B-pillar outer paneling (1) with body saw (areas R and Q).
 Courtesy of MERCEDES-BENZ USA
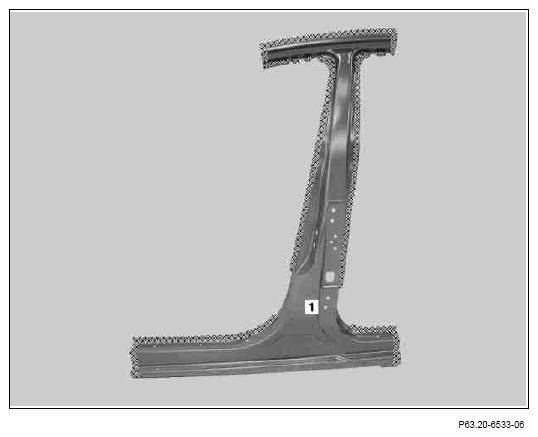
- Grind mating surfaces on B-pillar outer paneling (1) down to bare metal in cross-hatched areas using
round wire brush.
Grind spot weld flanges down to bare metal on both sides.
To prevent adhesion problems, do not coat bonding surfaces with zinc dust paint.
Observe pretreatment of bonding surfaces.
 Courtesy of MERCEDES-BENZ USA