Valve Seat
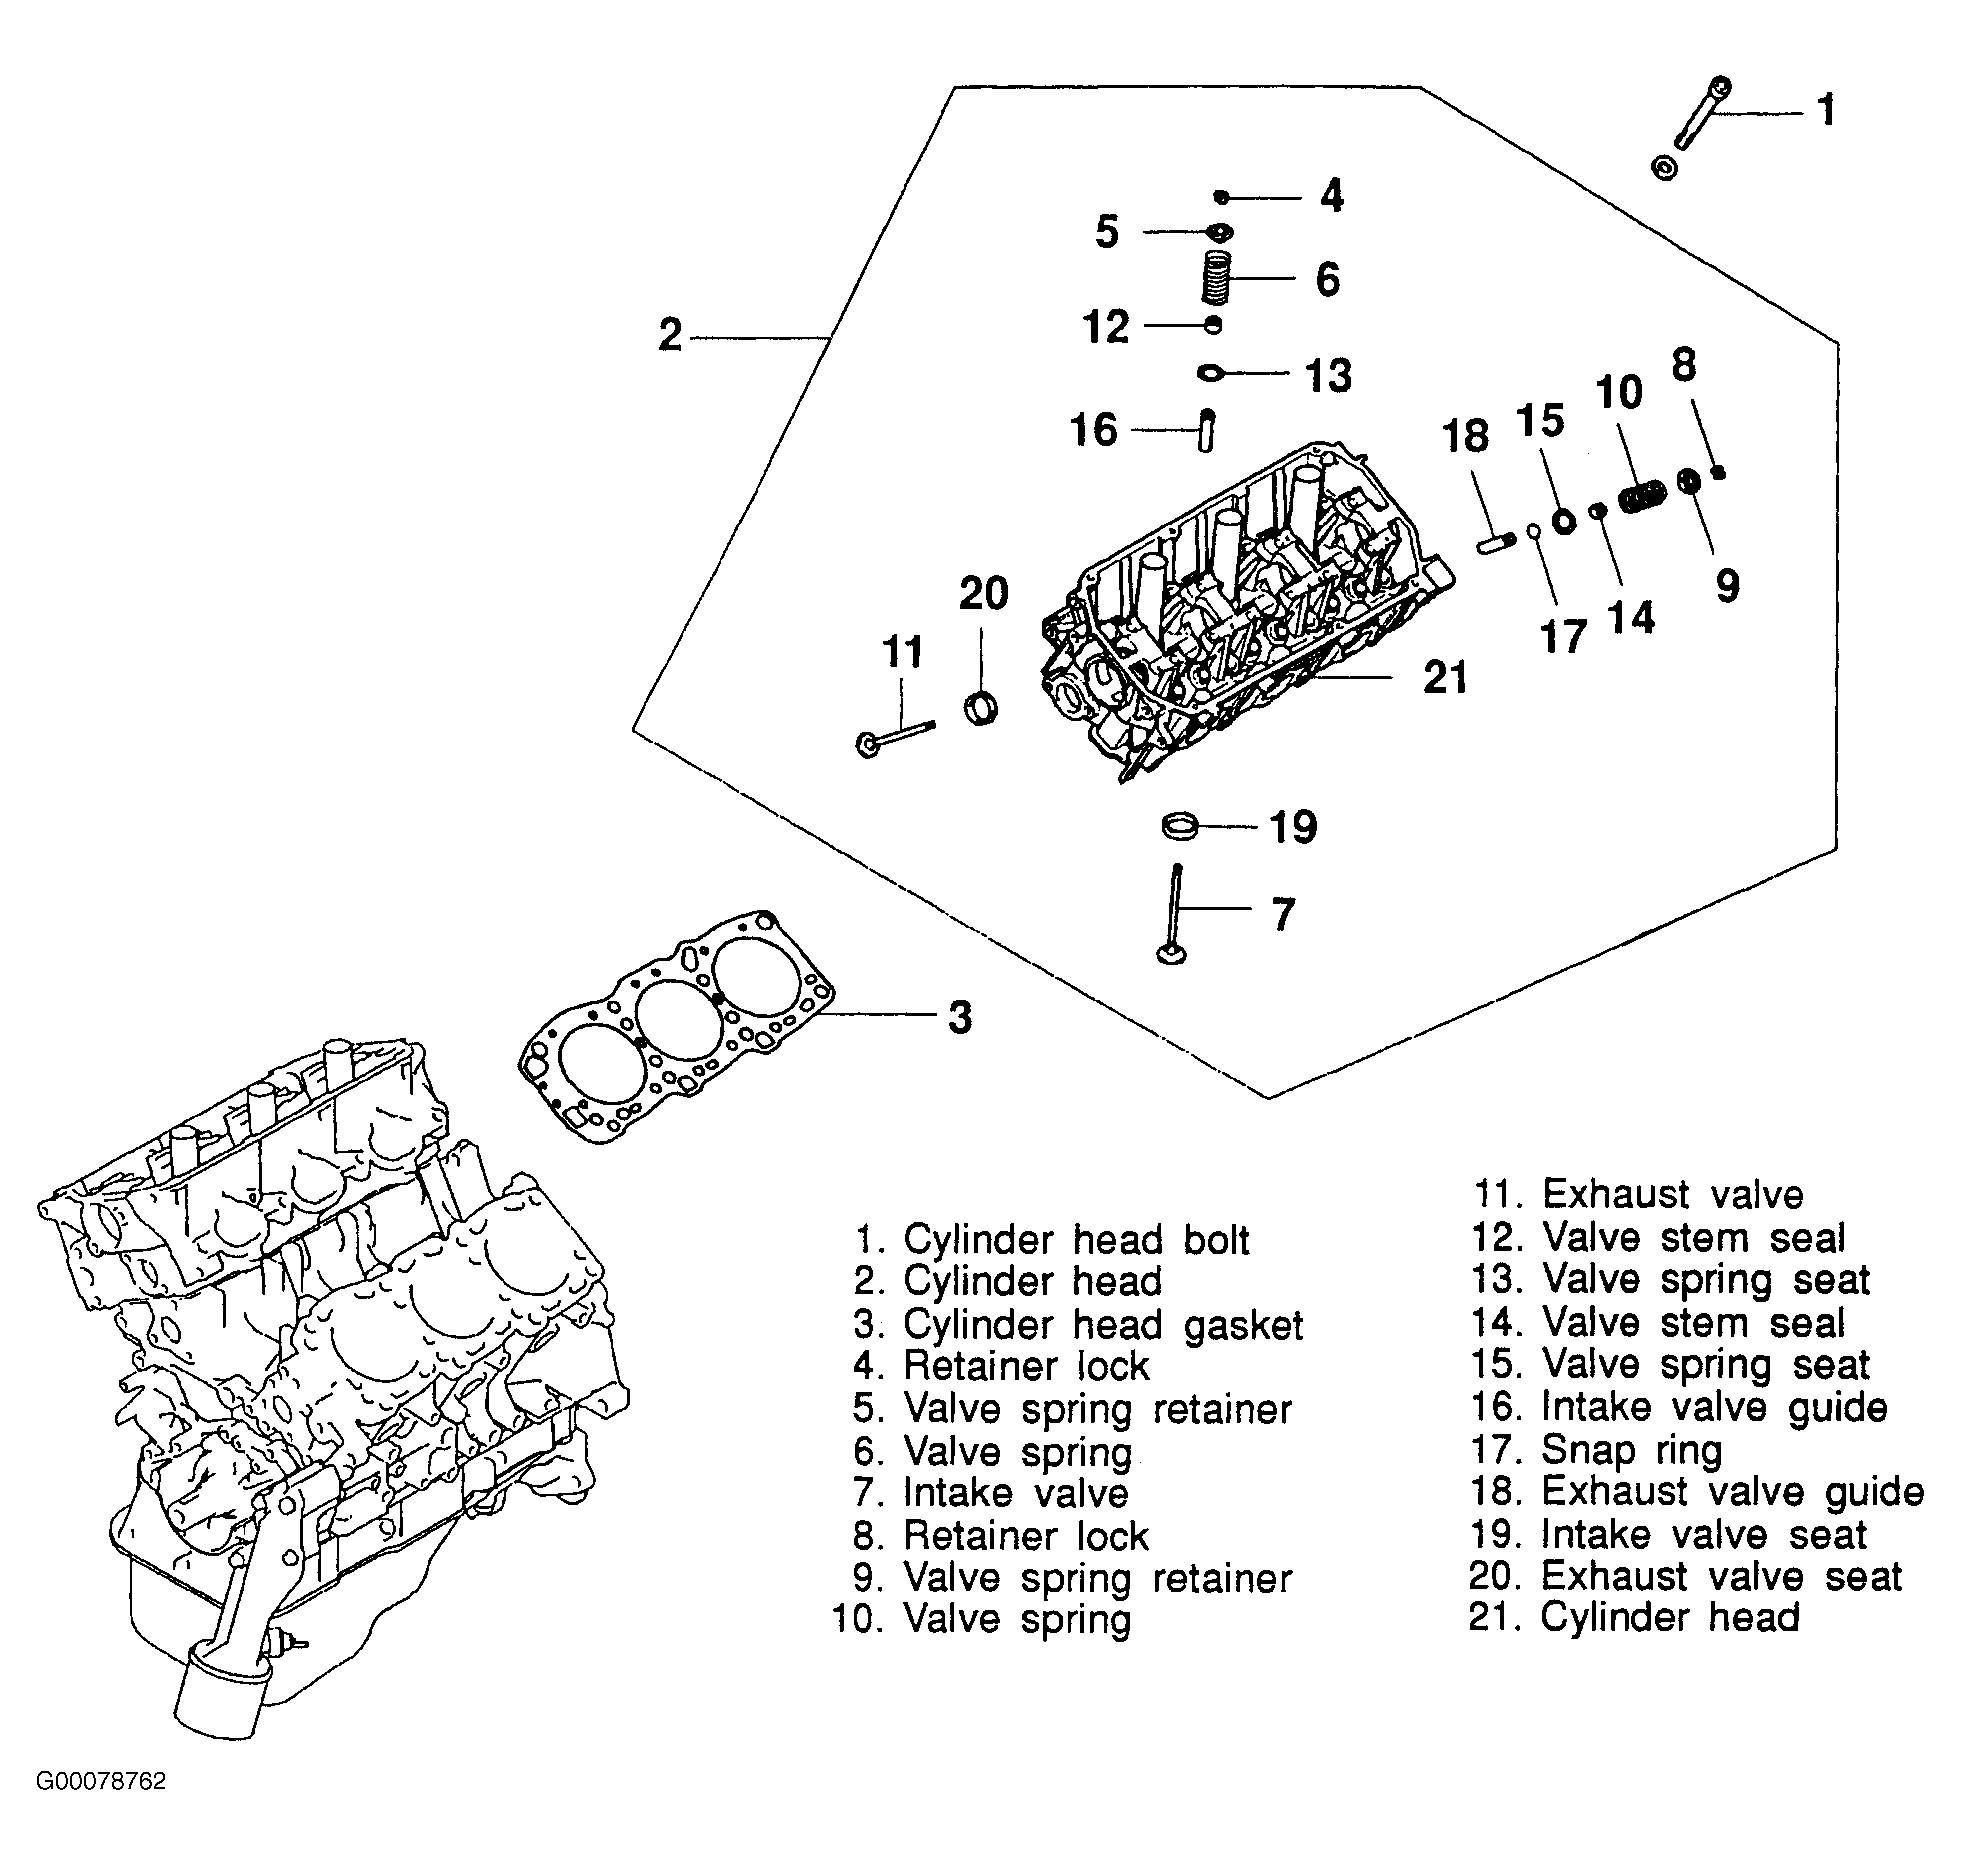
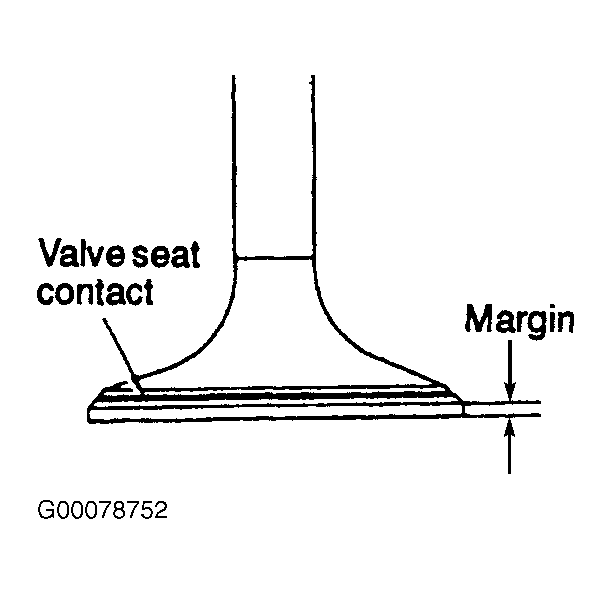
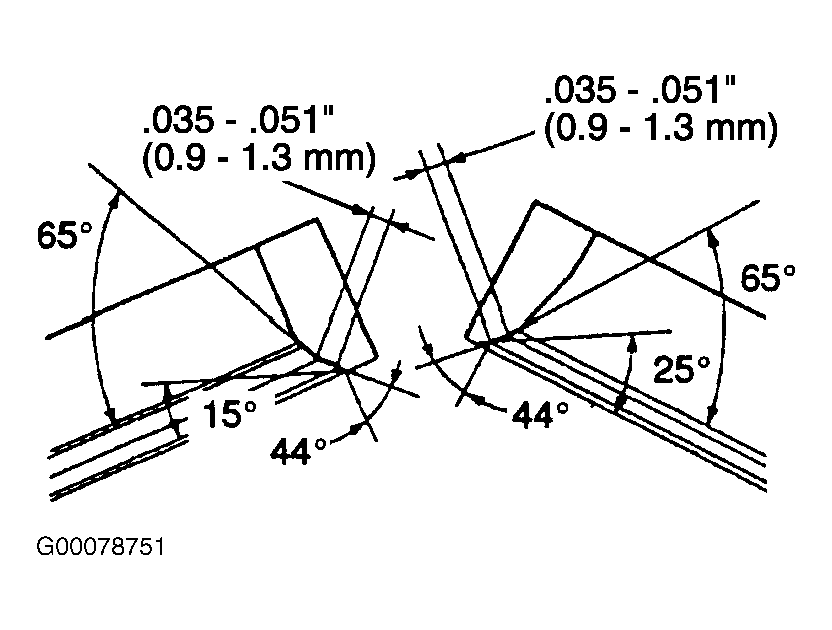
- Worn or burned valve seats can be reworked, provided proper angles and seat widths are obtained. See Fig 6. Before correcting valve seat, check for clearance between valve guide and valve end. If necessary, replace valve guide. Correct to obtain specified seat width and angle. After correction, lapp valve and valve seat with a lapping compound.
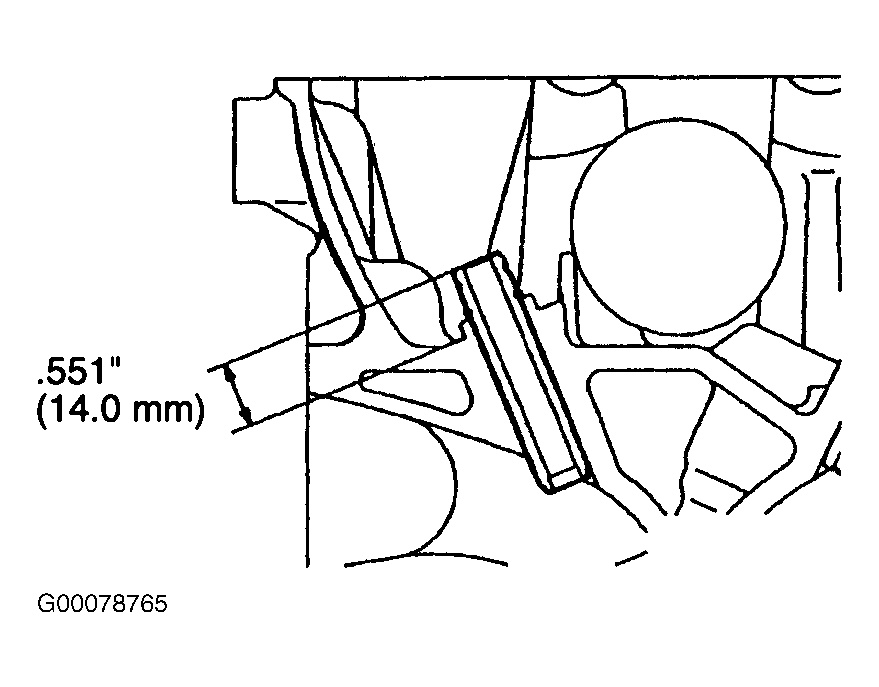
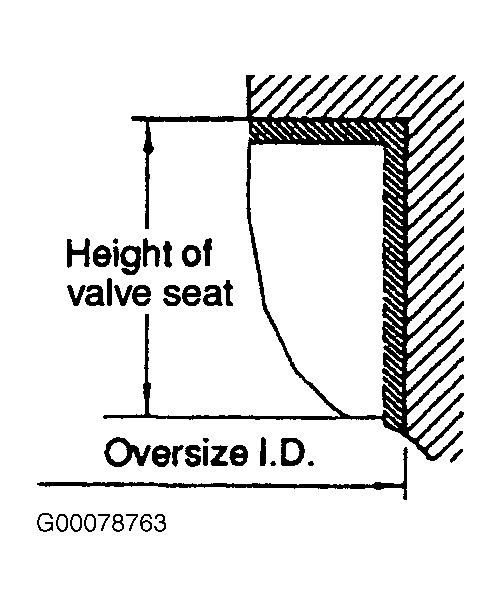
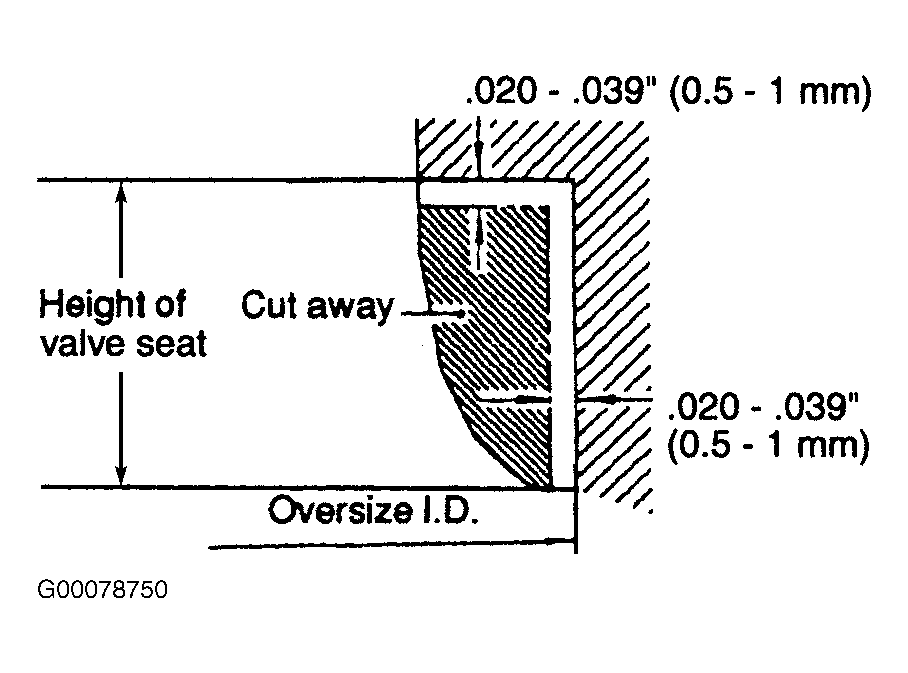
- To remove valve seat, cut seat in order to thin wall thickness. See Fig 7. Remove valve seat. Bore valve seat hole in cylinder head to oversize valve seat diameter. See Fig 3. Intake valve seats are available in 0.3 oversize, which is 1.3504-1.3516" (34.30-34.33 mm) or 0.6 oversize, which is 1.3622-1.3634" (34.60-34.63 mm). Exhaust valve seats are available in 0.3 oversize, which is 1.2520-1.2531" (31.80-31.83 mm) or 0.6 oversize, which is 1.2638-1.2650" (32.10-32.13 mm).
- Before installing valve seat, either heat cylinder head to about 482°F (250°C) or cool valve seat in liquid nitrogen. Using valve seat cutter, correct valve seat to specified width and angle.
 Courtesy of CHRYSLER CORP.
 Courtesy of CHRYSLER CORP.
 Courtesy of CHRYSLER CORP.
 Courtesy of CHRYSLER CORP.
 Courtesy of CHRYSLER CORP.
 Courtesy of CHRYSLER CORP.
 Courtesy of CHRYSLER CORP.